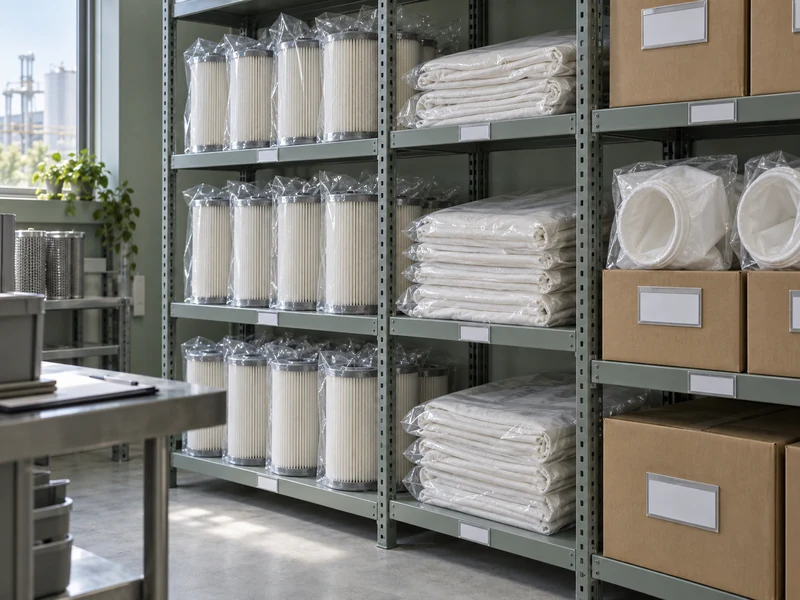
Set spare filter stock from expected demand during replenishment, complete changeout quantities, supply uncertainty, and the consequence of running out. Separate regularly consumed elements from rarely needed emergency spares. A single rule such as keeping one month of every item can leave a critical system exposed while tying up money in parts that are seldom used.
Which Items Belong in the Same Stock Group?
Group parts by verified interchangeability, not by a similar description in the purchasing system. Cartridge length, bag size, and micron label may conceal differences in connections, materials, or performance. A spare is useful only if it is approved for the equipment that needs it.
Create a parts-to-equipment map that identifies the installed quantity and approved alternatives. Include the relevant drawing or specification revision. This prevents a stock count from treating an obsolete or unqualified item as available protection.
Zonel Filtech’s liquid filter cartridge range includes different constructions and connections. When consolidating stock, verify the proposed common specification with the plant and supplier. Similar appearance should not be used as evidence that two duties can share one spare.
How Is Routine Demand Different from Emergency Demand?
Routine demand arises from planned or recurring changes and can often be related to production, operating hours, or processed volume. Emergency demand arises from damage, process upsets, or other irregular events. The two patterns need different planning assumptions.
Use actual issue records and work orders to distinguish them. A storeroom withdrawal may represent a planned change, a trial, an installation error, or a transfer to another site. Counting all withdrawals as identical consumption can distort the forecast.
Research on spare-parts inventory policies at MIT discusses the difficulty created by varying lead times and intermittent demand. That supports separating demand patterns before setting policy. It does not provide a universal stock level for filtration equipment.
What Is the Real Replenishment Lead Time?
Measure the time from the replenishment decision until the parts are available for approved use. Include internal purchasing approval, manufacturing, transport, receiving inspection, and any required release. Supplier dispatch time alone may understate the exposure.
Keep a record of actual lead times and their variation. A quoted average may not capture holiday closures, customs delays, or occasional manufacturing constraints. Use the level of uncertainty relevant to the part’s criticality.
If a trial or documentation review is required for a new supplier, that time belongs in the transition plan. Unqualified stock cannot automatically replace approved stock during a shortage. Establish alternatives before the primary supply runs out.
How Can a Basic Reorder Point Be Estimated?
For reasonably regular demand, begin with expected consumption during replenishment and add a justified safety allowance. Keep planned shutdown requirements separate when they create a large known demand. State the assumptions rather than hiding them inside one rounded number.
Consider an illustrative plant that uses 12 approved cartridges per week and has a four-week replenishment interval. Expected demand during that interval is 48 cartridges. If the plant selects an additional 24-cartridge allowance after reviewing variability and consequences, the illustrative reorder point is 72.
That example is not a recommended stock level. Another plant may need a different allowance because its lead time, demand pattern, or recovery options differ. The calculation is a starting framework to be checked against actual service experience.
| Planning Input | Evidence Needed | Effect on Policy |
| Regular consumption | Issue history linked to production | Estimates expected lead-time demand |
| Complete changeout quantity | Installed element count | Prevents unusable partial sets |
| Supply variation | Actual replenishment history | Informs the safety allowance |
| Failure consequence | Operational impact and contingency | Determines required protection |
| Usable stock status | Inspection and reservation records | Excludes unavailable inventory |
Why Do Complete Changeout Quantities Matter?
Some systems require a coordinated set of elements for a planned change. A shelf containing several loose spares may still be insufficient for that event. Record the complete set quantity and the plant’s approved replacement practice.
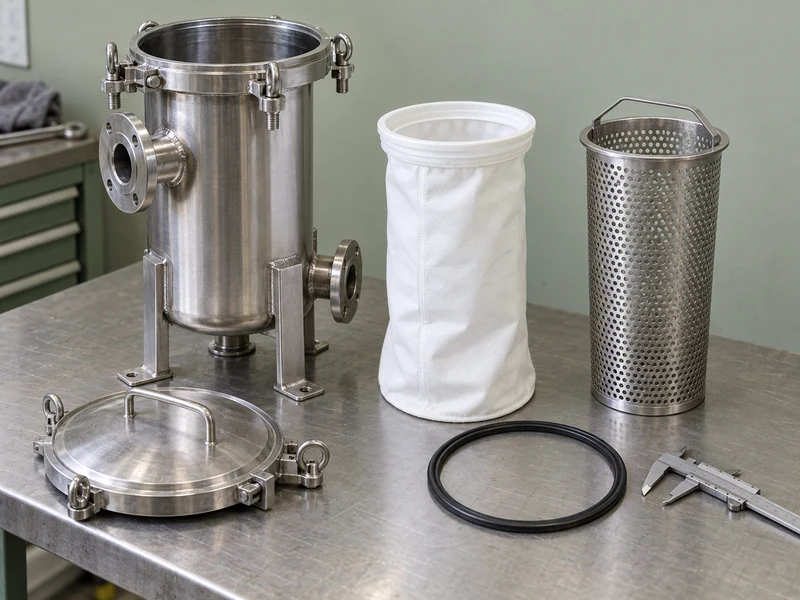
For a baghouse, the relevant planned work may involve a compartment or another defined group rather than an arbitrary number of bags. For a cartridge housing, the installed count and approved mixing policy matter. Follow the equipment and process requirements instead of assuming partial replacement is always acceptable.
When planning dust filter bag spares, identify the equipment and bag construction clearly. The site’s industrial filter bag size guide helps organize physical identification. Inventory planning then adds the quantity and timing needed for the actual maintenance event.
How Should Rare but Critical Spares Be Treated?
Evaluate the consequence of unavailability and the available contingency rather than relying only on annual consumption. A part with no recent withdrawals may still be essential if failure would stop a critical process and replacement takes a long time. Low usage does not automatically mean low importance.
Consider whether an approved spare can be shared across equipment, whether a standby unit exists, and whether an alternative operating plan is practical. These options may reduce the need for dedicated stock. Their availability should be verified rather than assumed.
Avoid applying a normal-demand formula mechanically to highly intermittent events. Sparse data may not support a precise statistical estimate. A documented engineering and operational review can be more honest than a sophisticated calculation built on uncertain inputs.
What Counts as Available Inventory?
Count stock that is physically present, correctly identified, approved, and not already committed to another job. Quarantined, damaged, expired where applicable, or unqualified material should be shown separately. A purchasing-system balance can otherwise overstate protection.
Track parts already reserved for a planned shutdown. If they remain in the general available balance, routine withdrawals may consume them before the shutdown begins. Reservation should be visible to both maintenance and purchasing.
Use an inventory-position calculation appropriate to the policy, including usable on-hand stock, confirmed incoming supply, and committed demand. Be explicit about how reservations and backorders are treated so they are not subtracted twice. The calculation should match the actual workflow.
How Should Planned Shutdowns Change the Order Plan?
Create a separate demand event for the shutdown and confirm its scope early enough to cover the real replenishment interval. Include the main elements and any required approved accessories. The quantity should reflect the work package, not a rough percentage added to normal consumption.
The site’s filter bag replacement guide provides maintenance context. Inventory planning should ensure the required approved parts are available when that procedure is scheduled. It does not replace the equipment-specific work instructions.
After the shutdown, reconcile issued, installed, returned, and rejected items. This improves the next forecast and identifies avoidable losses. Unreconciled returns are a common source of inaccurate stock records.
Which Performance Measures Improve the Policy?
Track stockouts, emergency purchases, actual lead time, obsolete stock, and the accuracy of reservations. Review these measures alongside consumption rather than celebrating low inventory in isolation. A lower stock value can be a poor outcome if it repeatedly interrupts production.
Distinguish a forecast error from an identification or transaction error. The correct parts may have been on site but inaccessible, incorrectly recorded, or reserved without visibility. Buying more stock will not necessarily solve those problems.
The site’s cartridge maintenance guidance can help classify the operating events behind consumption. This article uses those records to plan quantities; it does not duplicate storage and handling instructions. Keep the two responsibilities connected but distinct.
How Should New Equipment Enter the Stock Plan?
Before commissioning, confirm the installed element count, approved spare specification, expected initial changeout needs, and supplier replenishment assumptions. Early production may consume elements differently from mature operation because the process is still stabilizing. Treat commissioning demand separately rather than allowing it to distort the long-term forecast.
Assign ownership for updating the parts list after the final equipment configuration is accepted. Trial elements and superseded connections should not remain indistinguishable from approved spares. Reconcile the commissioning stock before routine replenishment begins.
When Should Stock Levels Be Reviewed?
Review the policy after changes in production, element specification, supplier lead time, or installed equipment. Also review it after a significant stockout or repeated emergency orders. A reorder point that once worked may no longer fit the current operation.
Set a regular review interval suited to the site’s purchasing cycle and criticality. During the review, confirm that approved alternatives remain valid and that obsolete part numbers are controlled. Retain the reason for each policy change.
Provide Zonel Filtech with the installed quantities, expected change schedule, approved specifications, and delivery constraints when discussing supply planning. Clear demand information helps align manufacturing and delivery with actual needs. The final stock decision should remain tied to the plant’s service requirement and measured supply exposure.